How to Source Wholesale Packing Tape Without Compromising Carton Seal Strength
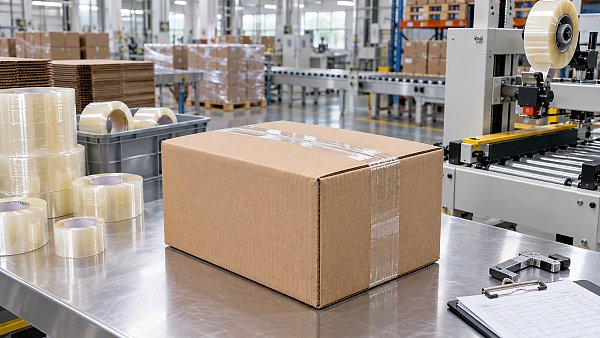
A carton that opens during handling rarely fails because the tape was visibly “cheap.” It usually fails because the tape specification was reduced to a roll price, while the actual sealing conditions were never defined. A procurement team may switch to a lower-cost wholesale packing tape, only to see case sealers struggle, tape lifting from recycled board, or cartons splitting along the centre seam after a temperature change. The resulting repacking, damage claims, and dispatch delays can erase the apparent savings quickly.
The practical answer is to source tape against the required seal system, not against roll width, length, or unit price alone. Define the carton, load, storage environment, application method, and acceptable seal performance before comparing suppliers. Then verify samples on the real cartons and, where relevant, on the actual packing line. This approach does not require buying the most expensive tape; it prevents buyers from paying for the wrong combination of backing, adhesive, and unwind characteristics.
Start with the carton and the failure mode
Packing tape works as part of a system. Its adhesive must wet and grip the carton surface, its film or paper backing must resist stretching or tearing, and the completed seal must hold when the carton flaps are under tension. A tape that performs well on a clean, new corrugated box may perform poorly on a lightweight board with a high recycled-fibre content, a dusty surface, or a moisture-affected finish.
Before requesting quotations for wholesale packing tape, identify what is actually happening when cartons fail. The visible symptom matters because it points to a different corrective action.
- Tape lifts cleanly from the carton: adhesion to the board is inadequate, often due to carton surface conditions, adhesive choice, low application pressure, or cold application.
- Tape remains attached but the backing splits or stretches: the backing grade, thickness, or tensile strength may be insufficient for the carton load or handling stresses.
- The carton tears beside the tape: the adhesive bond may be strong, but the board itself may be too weak for the load or closure pattern.
- The centre seam opens after stacking: flap tension, insufficient tape overlap, poor application pressure, or inadequate tape width may be contributing.
- Seals fail intermittently on an automated line: look beyond adhesive strength. Roll consistency, unwind force, machine settings, blade condition, and tape alignment can all be involved.
This distinction prevents a common purchasing error: specifying a stronger adhesive when the real weakness is the carton, or ordering thicker film when the problem is poor bonding to rough board.
Set the performance brief before asking for prices
A supplier can quote a tape accurately only when the request describes the working conditions. “Clear carton tape, standard grade” invites inconsistent offers because each supplier may interpret standard grade differently. Instead, build a short performance brief that procurement, packaging, and warehouse teams can all use.
Information that should be on the brief
- Carton dimensions, board construction, and whether the outer surface is virgin, recycled, coated, printed, waxed, or dusty.
- Typical and maximum gross carton weight.
- Contents that may shift, create internal pressure, or require reinforced closure.
- Sealing pattern: single centre strip, H-seal, double strip, or another method.
- Tape width and required overlap onto each carton flap.
- Manual dispenser, hand application, semi-automatic equipment, or fully automatic case sealer.
- Temperature and humidity at packing, during storage, and during expected transport.
- Whether cartons are opened and resealed, stored for long periods, or exposed to refrigerated or cold-chain transitions.
- Required format, including core size, roll length, colour, printing needs, and pallet delivery requirements.
Not every shipment needs the same specification. Light cartons of stable goods in a dry warehouse may be suitable for a cost-focused general-purpose grade. Cartons carrying denser goods, long export journeys, variable climates, or frequent manual handling need a more conservative selection. Splitting these applications into two or three tape specifications is often more economical than applying a premium grade to every carton or forcing one low-cost grade into demanding uses.
Choose adhesive chemistry for the operating environment
Adhesive type has a major influence on initial grab, bond development, temperature tolerance, and behaviour on different board surfaces. Product names vary by supplier, so procurement documents should request the adhesive family and the relevant performance data rather than relying only on trade descriptions.
There is no universal ranking in which one adhesive is always better. A tape with excellent initial tack may not be the right choice if it causes excessive machine noise or inconsistent release. Conversely, a tape with moderate initial grab may work reliably when cartons are clean, application pressure is adequate, and the bond has time to develop before transport. The correct question is whether the tape maintains a secure seal under the actual process and distribution conditions.
Do not treat film thickness as the whole strength specification
Buyers often compare polypropylene tape by microns because thickness is easy to state and easy to negotiate. It is relevant, but it is not a complete proxy for carton seal strength. Total thickness may include both film and adhesive, while suppliers may describe film gauge, total gauge, or a nominal grade differently. Two tapes with similar stated thickness can behave differently because of film formulation, adhesive coating weight, tensile properties, and manufacturing consistency.
Ask suppliers to clarify whether the quoted thickness is the backing film only or the finished tape. Request documented values for tensile strength, elongation at break, adhesion to steel or another stated test surface, and, where available, holding performance. These figures do not replace carton trials, because laboratory surfaces are not corrugated board, but they make comparisons more meaningful.
Tape width also affects closure strength. A narrow strip can be adequate on small, lightly loaded cartons with low flap tension. Wider tape gives more bonding area and provides a greater margin when carton flaps are uneven, board surfaces are rough, or loads place stress on the seam. That does not mean width should be increased automatically: a wider tape uses more material and may require adjustment to dispensers or machine heads. The required overlap and sealing pattern should drive the decision.
Run a controlled trial on representative cartons
A sample roll applied by hand to one empty carton is useful only as an initial screen. A proper buying trial should replicate the cartons, contents, closure method, and storage conditions that matter. It should also include samples from each shortlisted supplier, ideally identified by code rather than brand name during operational assessment.
- Use production-representative cartons. Include the lightest board, the roughest recycled surface, and the heaviest or most demanding pack configuration likely to be used.
- Apply tape under normal conditions. Use the intended dispenser or case sealer, standard tape tension, and normal operator practice. A tape should not be approved solely because it works with unusually careful hand application.
- Inspect immediately and after dwell time. Check whether edges lift, whether the adhesive wets the board, and whether the bond develops after the cartons sit under normal warehouse conditions.
- Assess practical handling. Stack cartons, move them through ordinary internal handling, and inspect seam integrity after realistic compression and movement. The purpose is to identify likely operational weaknesses, not to create an artificial performance claim.
- Record process observations. Note noise, telescoping rolls, adhesive build-up, roll breaks, poor cut-off, variable unwind, and operator complaints. These issues affect labour and line uptime even when the seal itself remains intact.
For high-value shipments, unusually heavy cartons, or routes with substantial temperature variation, expand the trial to include the expected environmental exposure. Packaging engineers or qualified testing providers may be appropriate where the closure has a safety, contractual, or product-protection consequence beyond routine warehousing.
Calculate landed sealing cost, not just tape cost
The lowest quoted price per roll can hide major differences in usable length, actual width, downtime, waste, and number of strips needed per carton. Compare offers on a common basis: cost per sealed carton under the required closure pattern. This makes a shorter roll or lower-performing tape easier to identify.
For each candidate, calculate the estimated tape consumption per carton using the actual strip length and number of strips. Then add expected material waste from roll changes, torn tape, machine set-up, and rejected seals. A grade that allows a secure single-strip closure may be more economical than a cheaper tape that requires a wider strip, a second strip, or frequent resealing.
Operational cost deserves equal attention in automated facilities. Inconsistent roll build can create tracking problems. Variable unwind can affect application tension. Excessively aggressive adhesive can leave residue on machine components, while weak or uneven coating can lead to random edge lifting. Ask the warehouse team to log these issues during trials rather than relying on a final yes-or-no opinion.
Qualify the supplier’s consistency, not only the sample
A sample may be acceptable while later deliveries vary in thickness, adhesive coating, roll length, or unwind behaviour. Procurement controls should therefore convert the approved trial into a clear supply specification. Include the product code, stated construction, acceptable dimensional tolerances, roll format, core size, packaging configuration, and agreed method for handling nonconforming goods.
It is reasonable to ask how the supplier manages batch identification and whether a delivery can be traced to a production batch. For recurring purchases, retain a reference roll from approved deliveries and investigate material changes when packing teams report a shift in performance. This is especially useful when carton board has also changed, because the cause may lie in the interaction between two materials rather than in the tape alone.
Supply resilience matters when tape is a line-critical consumable. Clarify lead times, minimum order quantities, stockholding arrangements, substitute-grade rules, and notification requirements before any specification change. A substitute tape should not be accepted simply because its width and colour match; it should meet the agreed performance brief or be trialled before broad release.
Warning signs during a cost-reduction exercise
Be cautious when a quotation is materially lower but provides only a roll dimension and a generic adhesive description. Other warning signs include unclear total thickness, no distinction between film and finished gauge, missing roll length tolerances, samples that differ from quoted stock, or a recommendation to use the same tape across cartons with very different weights and surfaces.
Another frequent mistake is reducing tape grade at the same time as changing carton board, closure pattern, or packing-line settings. When a problem appears, there is no reliable way to identify which change caused it. Stage changes where possible: establish a baseline, trial one variable, document the result, and then decide whether the saving is genuine.
A sound wholesale packing tape decision protects the carton seal without overspecifying every shipment. Define the real application, select adhesive and backing properties that fit it, validate the choice on representative cartons, and buy against a controlled specification. That sequence gives procurement teams a defensible cost comparison while keeping carton integrity where it belongs: as a requirement, not an assumption.
Search News
Hot Articles
- Stationery & UniformsHow to Source Wholesale Packing Tape Without Compromising Carton Seal StrengthSep 17, 2026
- Smart Campus TechHow to Source Educational Furniture Worldwide for Safe, Flexible Learning SpacesSep 16, 2026
- Arcade & VR MachinesHow to Choose Coin-Operated Pool Tables for Bars, Hotels, and Arcade VenuesSep 15, 2026
Popular Tags
Need ExpertConsultation?
Connect with our specialized leisureengineering team for procurementstrategies.
Recommended News
 Sep 17, 2026How to Source Wholesale Packing Tape Without Compromising Carton Seal StrengthWholesale packing tape sourcing guide: compare adhesive, backing, carton conditions, and real-world trials to reduce costs while maintaining reliable carton seal strength.● Institutional Buyer
 Sep 05, 2026How to Buy Geometry Sets in Bulk for Schools: A Practical Procurement ChecklistGeometry sets bulk buying guide for schools: compare safety, quality, compliance, packaging, supplier reliability, and total cost for smarter procurement.● Institutional Buyer
 Aug 31, 2026Microscope Slides Market Outlook: Demand Drivers, Segments, and Sourcing RisksExplore the microscope slides market: key demand drivers, product segments, quality risks, and sourcing strategies for reliable laboratory supply.● Institutional Buyer
 Aug 30, 2026Microscope Slides HS Code: How Importers Classify Laboratory Glass Slides CorrectlyMicroscope slides HS code guide: learn how to classify laboratory glass slides accurately, verify materials, avoid customs delays, and improve import compliance.● Institutional Buyer
 Aug 29, 2026How to Choose Graduation Tassels With Year Charms for Large School OrdersGraduation tassels with year charm: learn how to specify colors, materials, packaging, proofs, and delivery timelines for accurate large school orders.● Institutional Buyer
 Aug 11, 2026How to Choose Alphabet Educational Posters for Different Classroom Age GroupsAlphabet educational posters should match how each age group learns. Discover how to choose safer, clearer, curriculum-ready designs for preschool to primary classrooms.● Institutional Buyer
 Aug 05, 2026How to Evaluate a Marching Band Uniform Manufacturer for Quality and On-Time DeliveryMarching band uniform manufacturer selection starts with delivery risk. Learn how to compare quality, sizing, compliance, and capacity for reliable, on-time orders.● Institutional Buyer
 Jul 20, 2026How to Evaluate a Stationery Distributor for Bulk Office and School Supply PurchasingStationery distributor selection affects cost, delivery, and compliance. Learn how to evaluate suppliers for bulk office and school supply purchasing with confidence.● Institutional Buyer
 Jul 18, 2026How to Choose Custom Hotel Uniforms: Fabric, Branding, Comfort, and DurabilityCustom hotel uniforms guide: learn how to choose the right fabric, branding, comfort, and durability to improve staff performance, strengthen hotel image, and reduce long-term costs.● Institutional Buyer
 Jul 15, 2026How to Choose a Clear Pencil Cases Manufacturer for School and Retail OrdersClear pencil cases manufacturer selection made simple: learn how to compare quality, compliance, customization, pricing, and lead times for school and retail orders.● Institutional Buyer
 Jul 14, 2026How to Evaluate a Hole Punches Wholesale Supplier for Quality, MOQ, and Lead TimeHole punches wholesale supplier selection starts with quality, MOQ, and lead time. Learn practical checks, warning signs, and sourcing tips to reduce risk and buy smarter.● Institutional Buyer
 Jul 13, 2026Wholesale Erasers and Sharpeners: How to Compare Materials, Packaging, and MOQWholesale erasers and sharpeners buying guide: compare materials, packaging, and MOQ to cut risk, improve quality, and choose suppliers with better value.● Institutional Buyer
 Jul 10, 2026Custom Housekeeping Uniforms: What Fabrics and Features Hold Up in Daily Hotel Use?Custom housekeeping uniforms that last: discover the best fabrics, stretch, stain resistance, and hotel-ready features to cut replacement costs and keep staff polished daily.● Institutional Buyer
 Jul 08, 2026Fast Warm Up Laminator Buying Guide: Speed, Film Thickness, and Use Case ExplainedFast warm up laminator buying guide covering warm-up speed, film thickness, and real use cases. Compare specs, avoid buying mistakes, and choose the right model with confidence.● Institutional Buyer
 Jul 08, 2026How to Choose School Supplies for Campuses by Grade Level, Budget, and Daily UseSchool supplies for campuses made simple: learn how to choose by grade level, budget, durability, and daily use to reduce waste, improve sourcing, and support every classroom.● Institutional Buyer
 Jul 05, 2026How to Choose Branded Office Stationery for Corporate Use and Budget ControlBranded office stationery buying guide: learn how to balance quality, customization, supplier comparison, and budget control for consistent branding and smarter corporate sourcing.● Institutional Buyer
 Jul 01, 2026Paper Guillotines Buying Guide: Manual vs Electric, Cut Size, and Safety FeaturesPaper guillotines buying guide covering manual vs electric models, cut size, and safety features. Compare costs, productivity, and key specs to choose the right machine.● Institutional Buyer
 Jun 29, 2026Bingo Cages and Balls: Sizes, Materials, and What Affects Game VisibilityBingo cages and balls guide: compare sizes, materials, contrast, and durability to improve visibility, fairness, and long-term value in commercial and event play.● Institutional Buyer
 Jun 25, 2026School Uniforms in Europe: Materials, Sizing, and Compliance Points for Bulk OrdersSchool uniforms Europe sourcing guide: compare materials, sizing accuracy, and EU compliance points for bulk orders to reduce risk, improve durability, and choose suppliers with confidence.● Institutional Buyer
 Jun 23, 2026Wholesale Playing Cards Casino Buying Guide: Paper Stock, Finish, Security, and MOQWholesale playing cards casino buying guide covering paper stock, finish, security features, and MOQ. Compare suppliers smarter, reduce sourcing risk, and choose casino-grade decks with confidence.● Institutional Buyer
 Jun 22, 2026Eco Friendly Office Stationery: What to Check Before Buying for Daily Business UseEco friendly office stationery buying guide for businesses: learn how to check materials, certifications, durability, supplier reliability, and total cost before choosing daily office supplies.● Institutional Buyer
 Jun 21, 2026How to Choose Custom Promotional Pens for Trade Shows, Schools, and Corporate GiveawaysCustom promotional pens: learn how to choose the right styles for trade shows, schools, and corporate giveaways with tips on quality, branding, durability, and sourcing.● Institutional Buyer
 Jun 16, 2026Microscope Slides Wholesale Buying Guide: Glass Types, Sizes, and MOQ FactorsMicroscope slides wholesale buying guide covering glass types, standard sizes, MOQ factors, and quality risks—compare smarter, reduce waste, and choose reliable bulk supply.● Institutional Buyer
 Jun 12, 2026How to Choose Wholesale Playing Cards for Casino Use: Materials, Finish, and MOQWholesale playing cards casino buyers: compare materials, finish, print quality, security features, and MOQ to reduce cost, improve durability, and choose a supplier casinos can trust.● Institutional Buyer